Análisis exhaustivo de la concienciación y las prácticas de seguridad en las operaciones de limpieza con hidrolimpieza a ultra alta presión (UHP)
17 de agosto de 2026
Intercambio de experiencias sobre la construcción y puesta en marcha de proyectos de limpieza industrial con chorro de agua a ultra alta presión.
5 de septiembre de 2026Selección del diámetro del tubo del intercambiador de calor para la limpieza industrial mediante chorro de agua a alta presión y ultra alta presión (UHP)
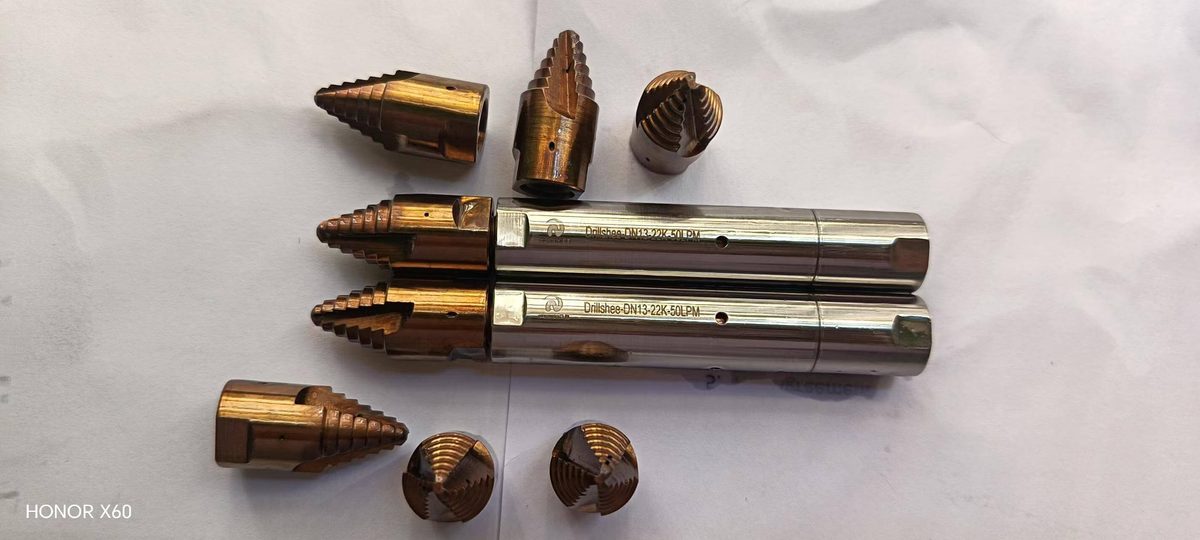
In high-pressure (HP) and ultra-high-pressure (UHP) industrial cleaning Water-Blaster applications, heat exchanger cleaning constitutes a critical maintenance process. Among the key technical parameters governing cleaning efficacy, tube internal diameter selection is particularly decisive—not merely as a geometric constraint, but as an integral factor influencing nozzle hydraulics, tool deployment mechanics, and overall process reliability.
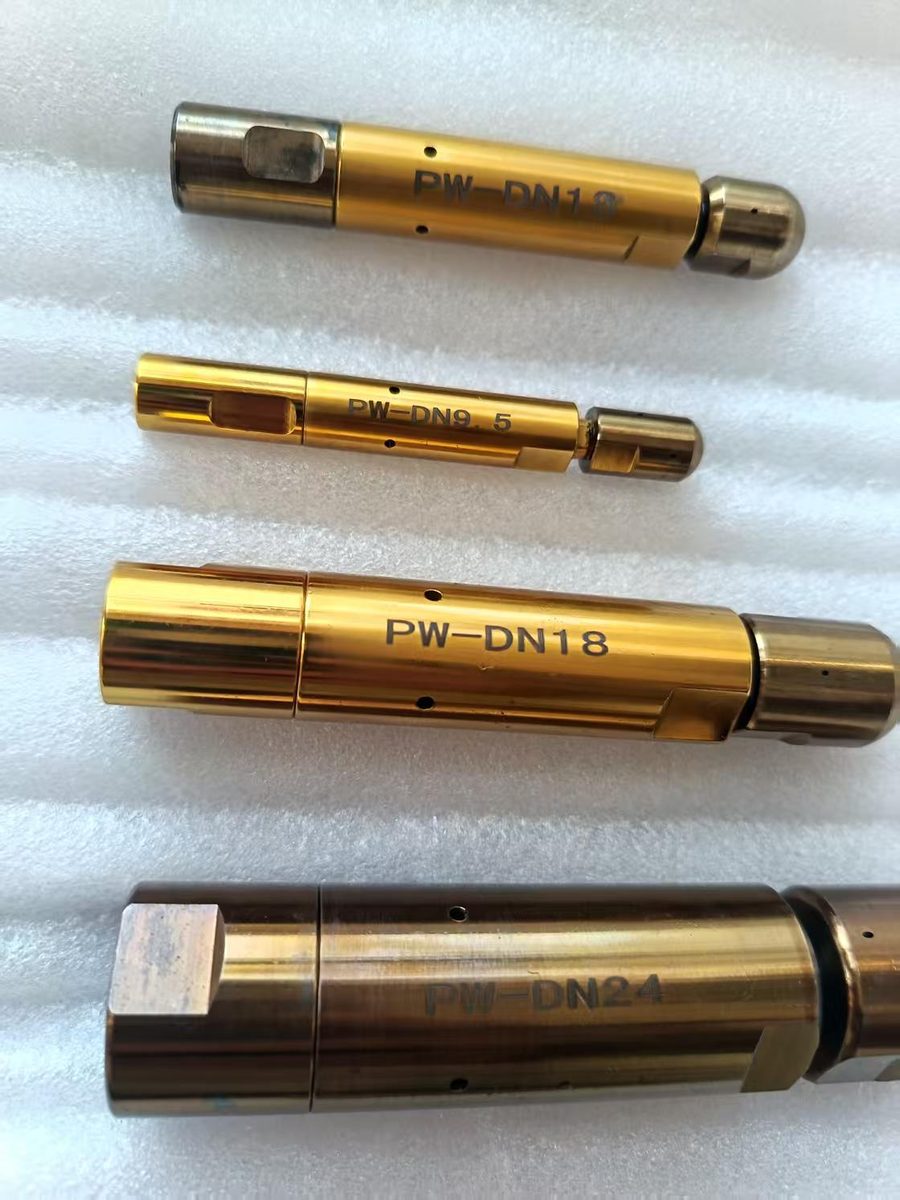
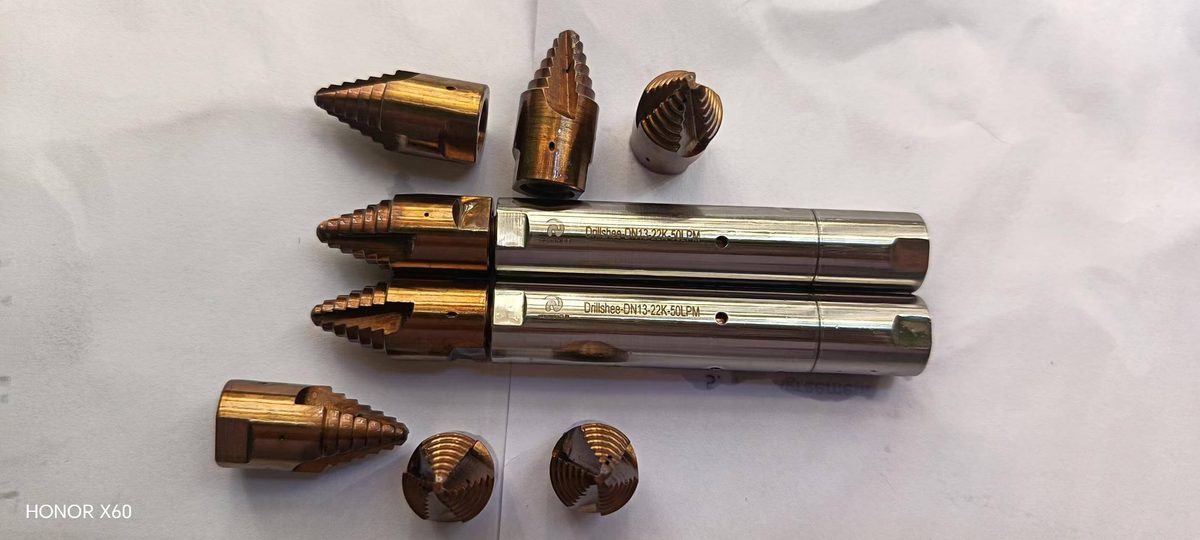
Effective cleaning of tube bundles requires systematic alignment of multiple interdependent variables: operating pressure and flow rate, Limpieza de tuberías petroquímicas Boquillas orifice diameter, hose coupling specifications, and Boquilla de chorro de agua a ultra alta presión configuration—including jet orientation.
Specifically, forward-directed jets primarily serve to dislodge and fragment obstructions; radially oriented (lateral) jets maximize wall shear stress for deposit removal;
and rearward-directed jets influence tool propulsion dynamics and facilitate transport of dislodged debris toward the outlet. Consequently, nozzle compatibility with tube geometry alone does not guarantee cleaning performance: a nozzle capable of physical insertion may prove ineffective against specific deposit types—such as loose particulates, viscous oil films, or consolidated blockages—or fail to meet required cleaning time-frames and quality standards.
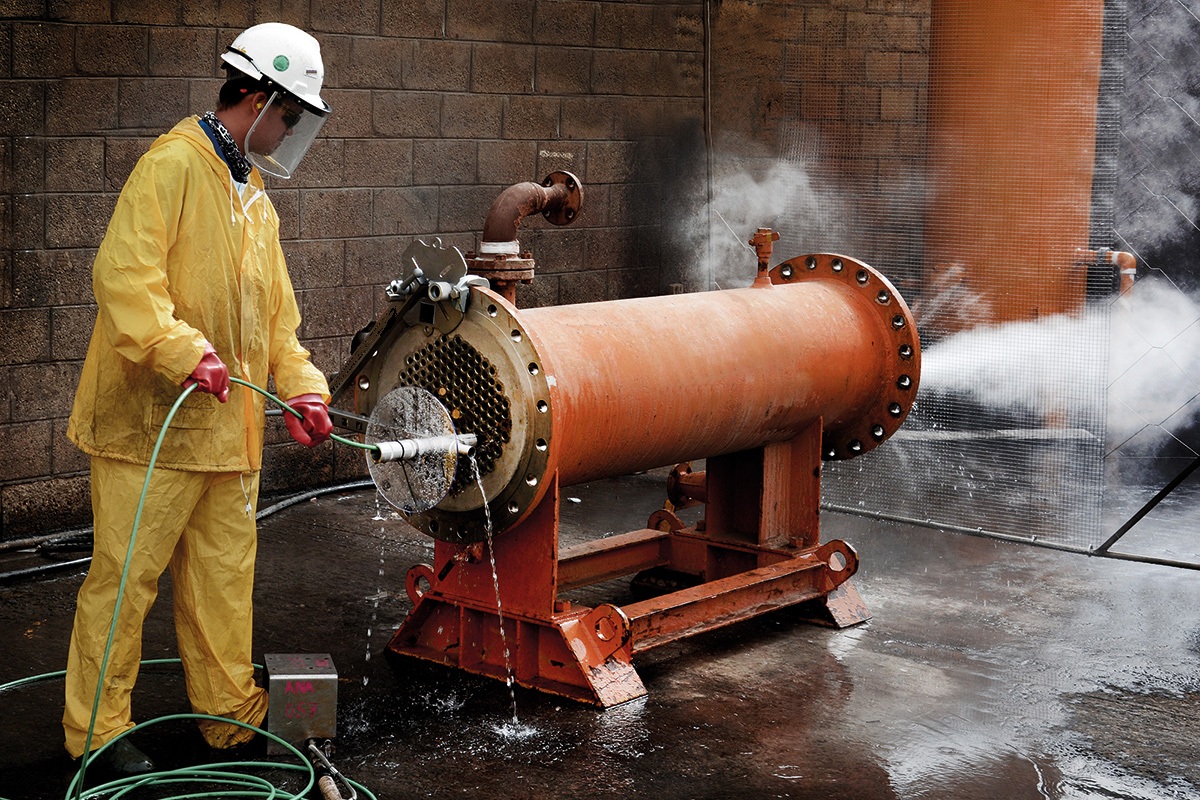
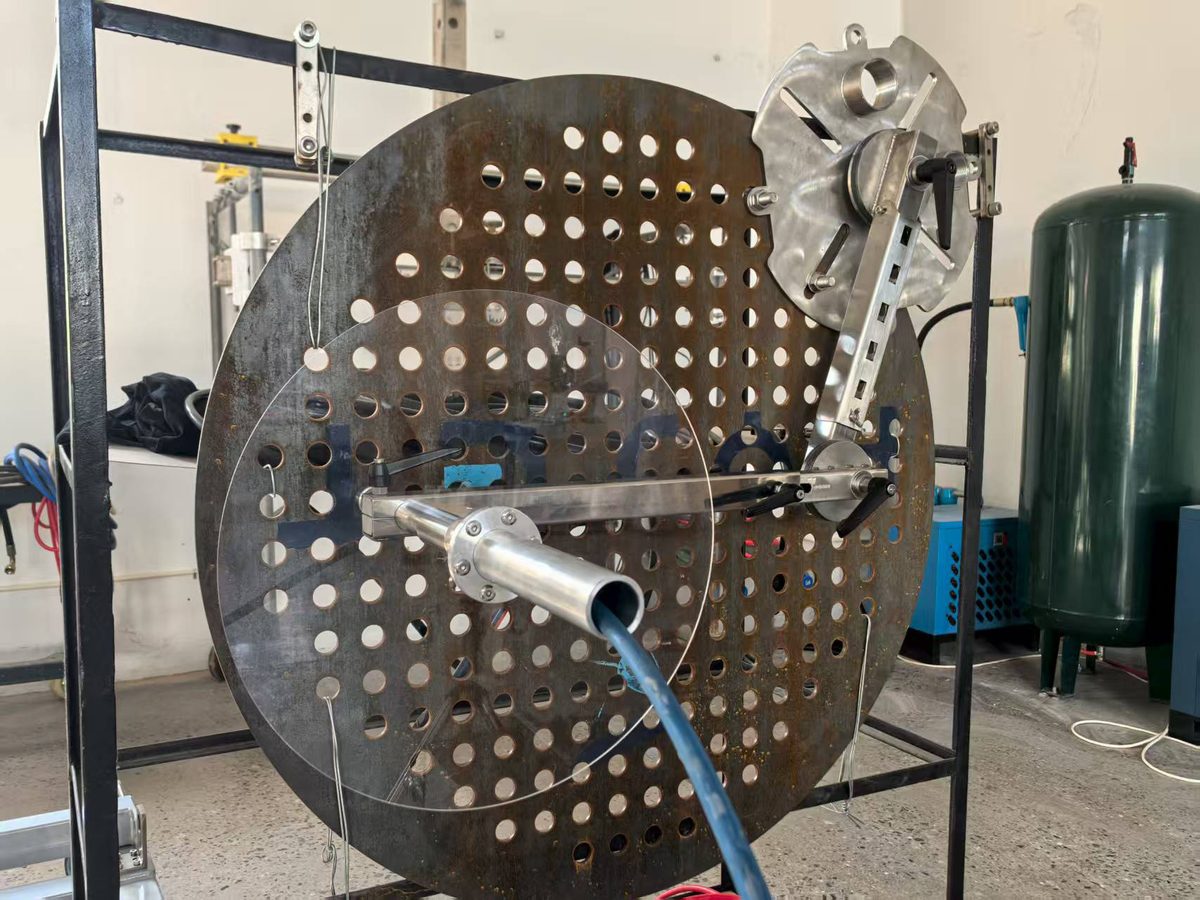
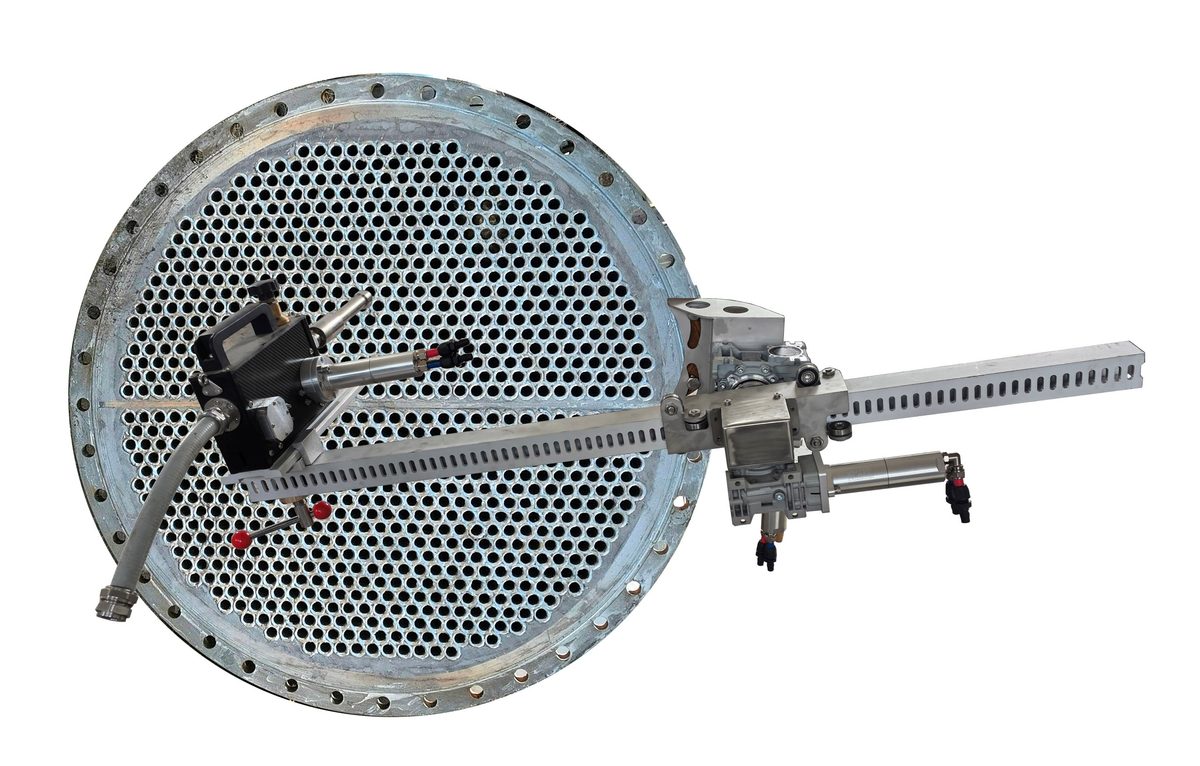
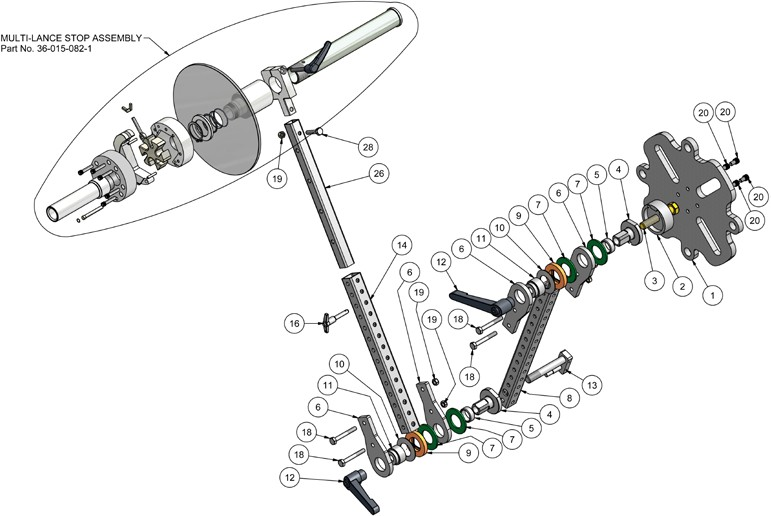
Further complicating selection are numerous site-specific and structural variables: minimum straight-tube inner diameter; presence and radius of curvature in bent tubes; tube length; available access space at the inlet; tube sheet layout (e.g., triangular vs. square pitch); wastewater recovery capability; hose feed mechanism (e.g., motorized push-pull vs. manual feed); and safety isolation requirements.
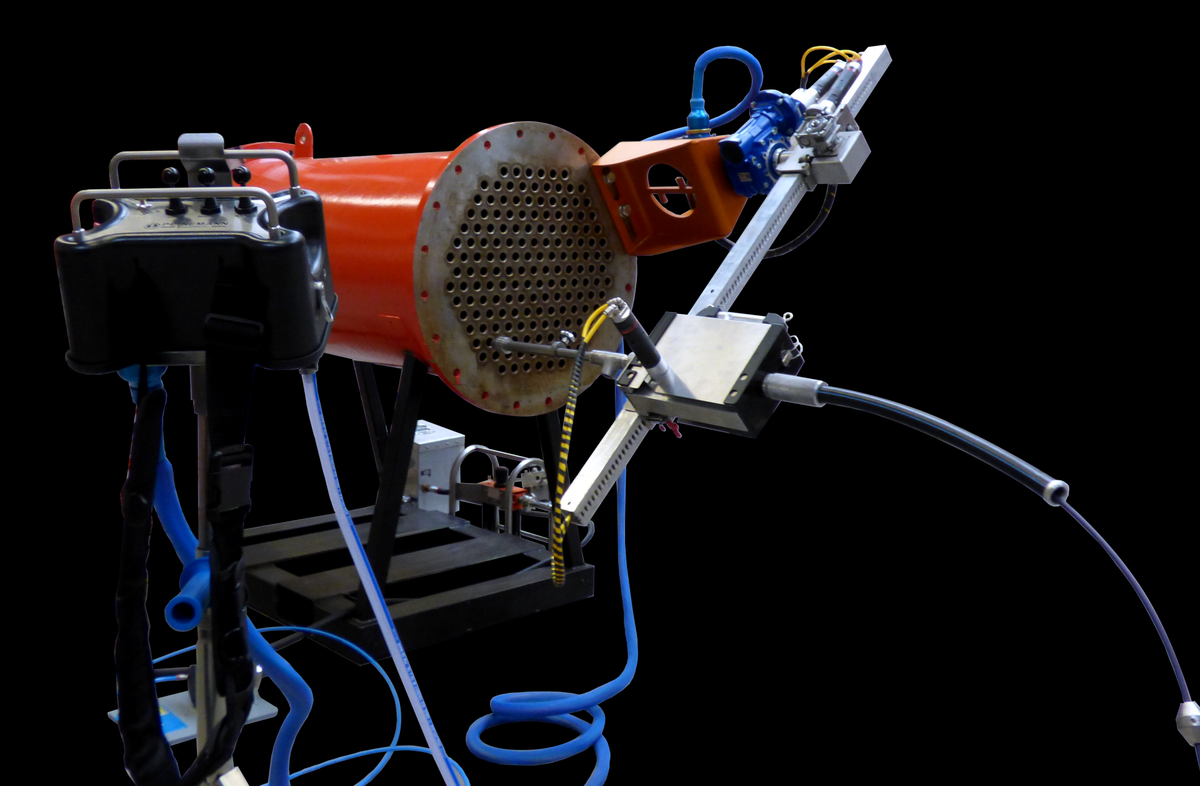
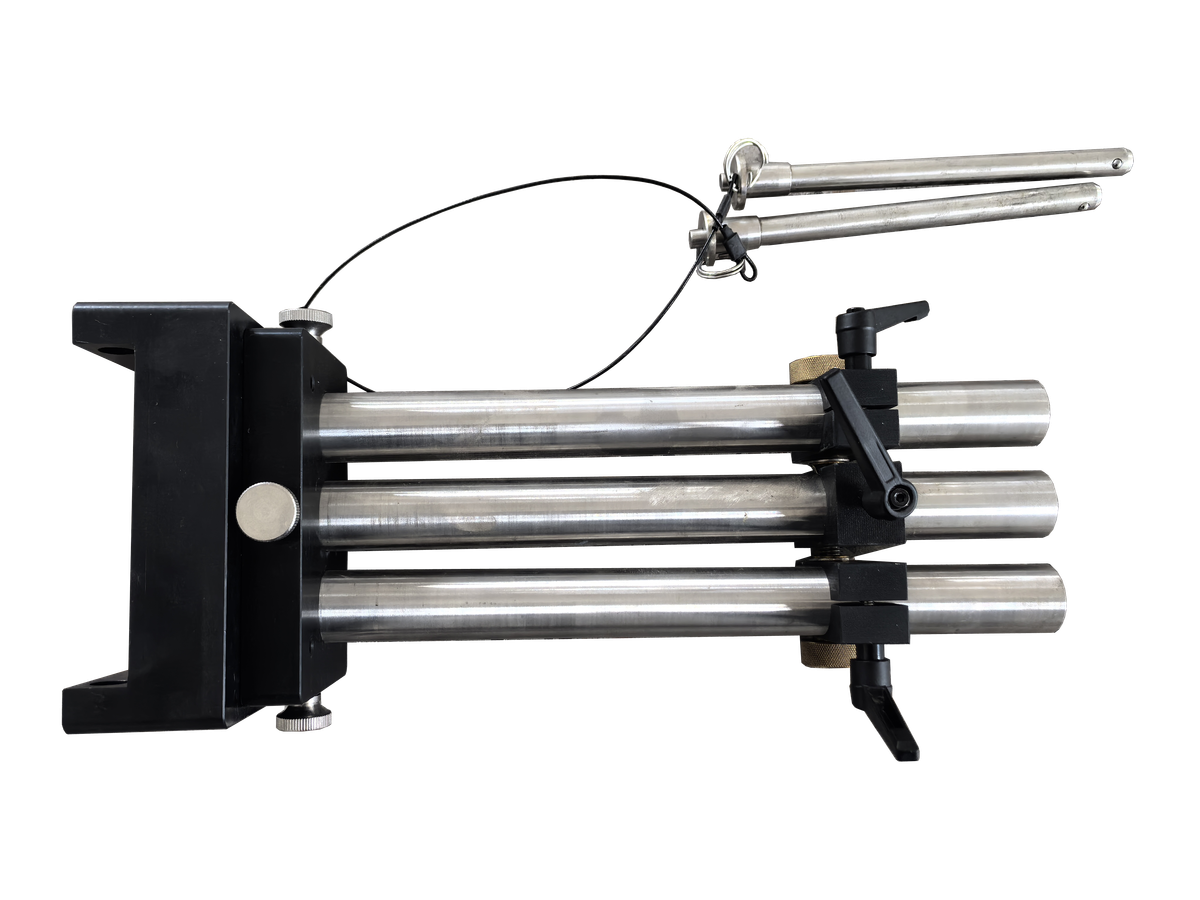
When procurement specifications provide only nominal pipe diameter and target pressure, suppliers can only conduct empirical nozzle trials—introducing uncertainty and potential rework. A robust engineering approach therefore mandates comprehensive data collection and analyse the need before make the final purchase decision, including:
• Minimum internal diameter (straight and curved sections);
• Tube length and curvature profile;
• Deposit type and severity (e.g., % blockage, composition, adhesion strength);
• On-site access constraints and workflow limitations;
• Objective pass/fail criteria for tube qualification (e.g., post-cleaning inspection method, residual deposit threshold, flow restoration target).
Crucially, successful cleaning demands concurrent optimization—not sequential consideration—of jet directional, volumetric flow rate, hose propulsion strategy, and quantifiable acceptance criteria, all calibrated to the actual service conditions.